Vacuum Formers
Two vacuum formers I built to make the capstone UAV's skin in-house: a full-size machine that formed 2 × 4 ft PETG sheets, and a scaled-down prototype used to test a better forming surface.
- FULL SIZE 2 × 4 FT
- PROTOTYPE 18 × 18 IN
- HEATER LIMIT 10 A @ 120 V
- VACUUM SHOP VAC

Objective
Form the capstone UAV's transparent PETG skin in-house at full 2 × 4 ft sheet size, with a machine that runs safely from a standard wall outlet.
What I made
- Built both vacuum formers: the full-size 2 × 4 ft machine and the 18 × 18 in prototype.
- Designed the heating element as an array of heating elements salvaged from toasters, and did the circuit math to cap its current draw at 10 A so it could run on a standard 120 V outlet.
- Tuned the heating element for forming.
- Designed the mold-making process and carried out the vacuum forming of the airframe skins.
Process & iteration
The full-size former came first, sized to form PETG sheets at 2 × 4 ft for the aircraft's skin. Its heating element is an array of heating elements taken from toasters. Because it had to plug into an ordinary wall outlet, I worked out the circuit so the whole array stays at or below 10 A of draw on a standard 120 V circuit. Both machines use a shop vac as the vacuum source.
While the full-size machine was being built and tested, I built a scaled-down 18 × 18 in former. It served two purposes: a test bed for forming over fine steel mesh instead of pegboard, and a demo that the team showcased at a science fair alongside the full-size machine. After that testing, the forming surface was switched from pegboard to fine steel mesh. The iteration history, from pegboard prototypes to the final steel-mesh configuration, is recorded in the vacuum-forming iteration matrix below.


Evidence
Vacuum-forming iteration matrix
| Version | Vacuum surface | Plastic used | Mold design | Plastic lower method | Form quality | Degree of mold degradation | Form consistency |
|---|---|---|---|---|---|---|---|
| Prototype 1 | Peg board | PVC | 3D print | Manual, unsupported | Med | High | Med |
| Prototype 2 | Peg board | PVC | 3D print, plaster fill | Manual, unsupported | Med | Low | Med |
| Prototype 3 | Peg board, more holes | PETG | 3D print, plaster fill | Manual, unsupported | Med | Low | Med |
| Prototype 4 | Peg board, more holes | PETG | 3D print, plaster fill | Manual, unsupported | Med | Low | Med |
| Final | Steel mesh | PETG | 3D print, plaster fill | Manual, supported | High | Low | High |
View the original spreadsheet screenshot
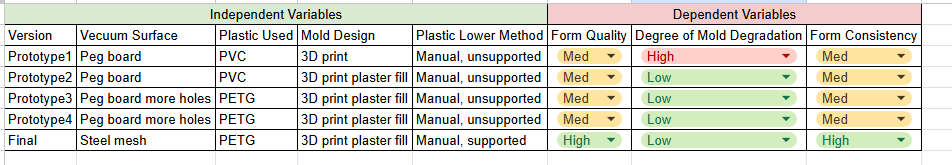
The vacuum-forming matrix shows the prototypes moving from PVC to PETG and from a peg-board to a steel-mesh vacuum surface across five iterations; the final entry rates high for form quality and consistency and low for mold degradation.
Limitations
This table is transcribed directly from the original spreadsheet screenshot linked above. The "Vacuum surface" column heading corrects a typo in the source image's own header text; no other values are altered.
Heater circuit
| Quantity | Value | Basis |
|---|---|---|
| Supply voltage | 120 V | Standard U.S. wall outlet |
| Maximum current draw | 10 A | Design limit set by the circuit math |
| Maximum power | 1,200 W | Derived: P = V × I at the 10 A limit |

Limitations
The 1,200 W figure is the theoretical maximum implied by the 10 A design limit, not a measurement.
Result
The full-size former produced 2 × 4 ft PETG sheets used for the capstone UAV's skin, and the prototype served as the test bed for the switch from pegboard to a fine steel-mesh forming surface. Both machines were shown together at a science fair.